Soluzioni / Desulfurization plants
Desulfurization plants
Business Unit: Process Analyzer
In the refining of petroleum products, an important stage of product treatment is the removal of sulfur, which by law must not exceed thresholds that vary from product to product and from state to state.
Opportunities
In any case, the plant must be calibrated according to the initial sulfur content present in the sample and the final sulfur content required. The process therefore requires monitoring of the total sulfur and certain chemical characteristics of the sample and of the components used at various points in the plant itself, including the humidity in the make-up hydrogen and the hydrogen sulfide in the sour gas exiting the amine plant.
Solution
Socrate S.p.A. offers a complete range of products for monitoring the entire system.
Socrate S.p.A. can support you
Are you interested in this product?
Products
The analyzer is based on QCM technology, ideal for process gases and applications in dehydration plants. Thanks to the internal NIST-traceable humidity generator, it does not require external calibration gas for reliable and accurate measurement guaranteed over time. The additional dryer allows the detection limit to be lowered up to ten times compared to standard QCM technology.
L'analizzatore si basa sulla tecnologia QCM con limite di rilevazione di 0,1 ppm, ideale per applicazioni con gas di processo, gas tecnici e gas naturale. Grazie al generatore di umidità interno tracciabile NIST non necessita di gas di calibrazione esterno per una misura affidabile e precisa garantita nel tempo
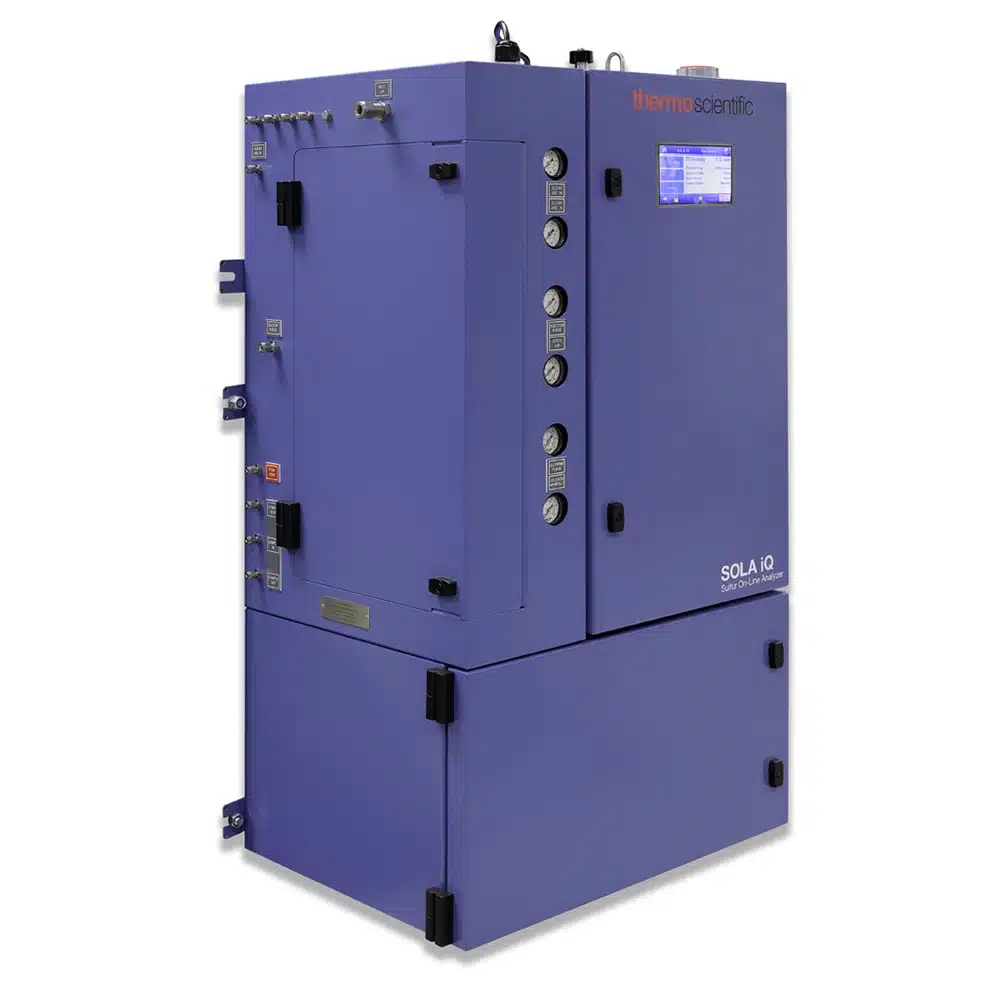
Total sulfur analyzer in liquid hydrocarbons, even at high viscosity, based on X-ray technology, suitable for monitoring sulfur in the range from 0.02 to 6%.
H2S (and H2) analyzer on Quench tower and Top Absorber for TGTU in Sulfur Recovery Plants. Equipped with a specific probe (ASR), it allows the sample to be returned directly to the process.
Total Sulfur Analyzer based on PUVF technology for measuring sulfur content in hydrocarbon products. The presence of a 1100°C pyrolyzer ensures complete oxidation of all sulfur compounds, converting them into SO2, which is then measured by a UV fluorescence photometer.
Fill out the form
You will be contacted within 24 hours.