The Sulfur Recovery Unit (SRU) is an essential plant for recovering sulfur compounds present in gas and oil, which are separated from the crude product during the refining process.
Opportunities
The plant's performance is essential for reducing sulfur emissions into the atmosphere, while also providing an economic benefit by reselling the recovered elemental sulfur for agricultural, industrial, and pharmaceutical uses.
Solution
Thanks to the use of analytical systems specifically engineered for these complex and delicate applications, it is possible to increase plant performance up to 99.97%. Socrate S.p.A. has been marketing complete and integrated solutions for this purpose for over 30 years.
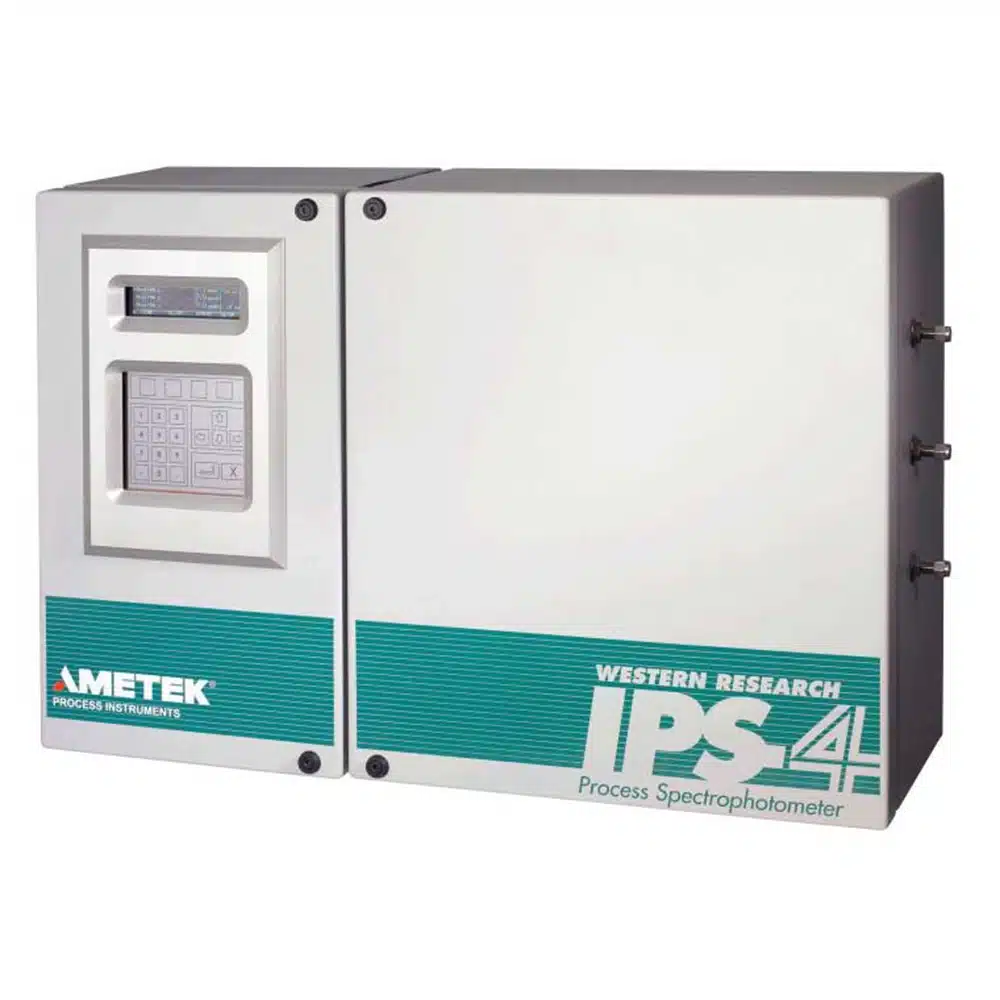
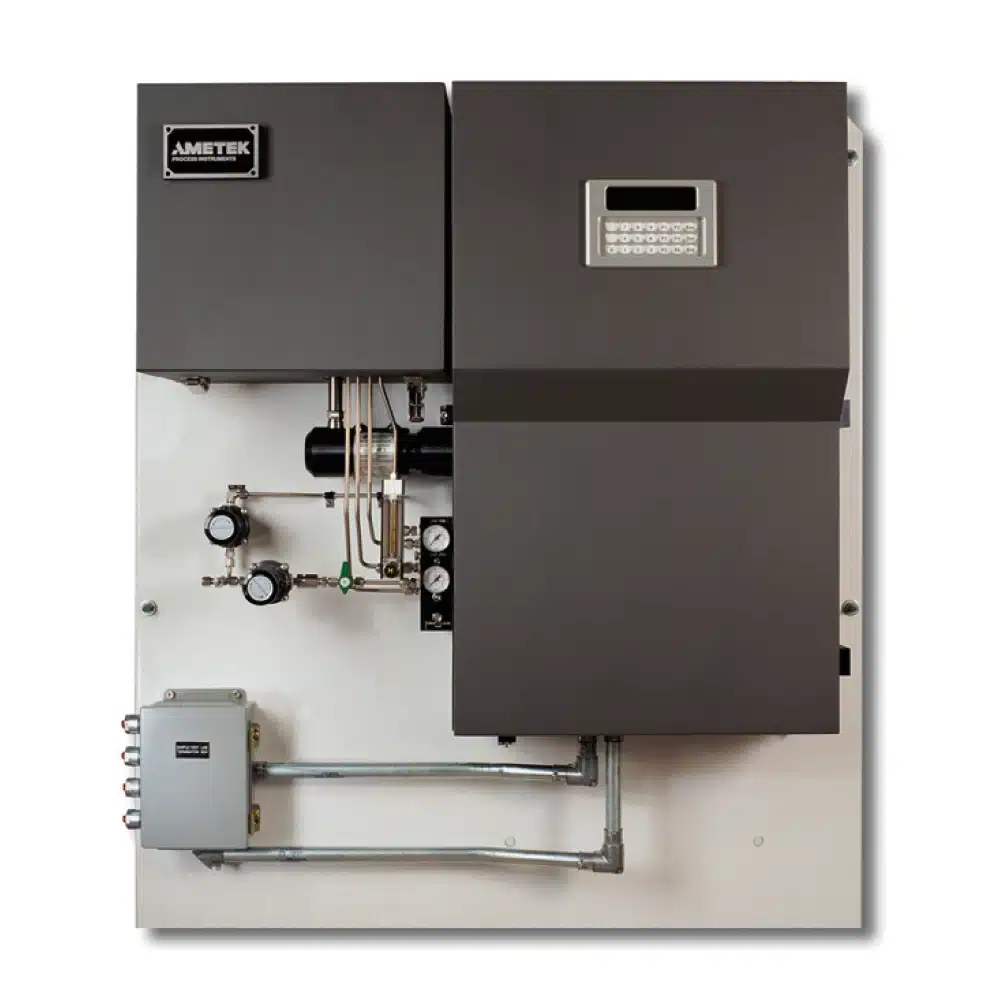
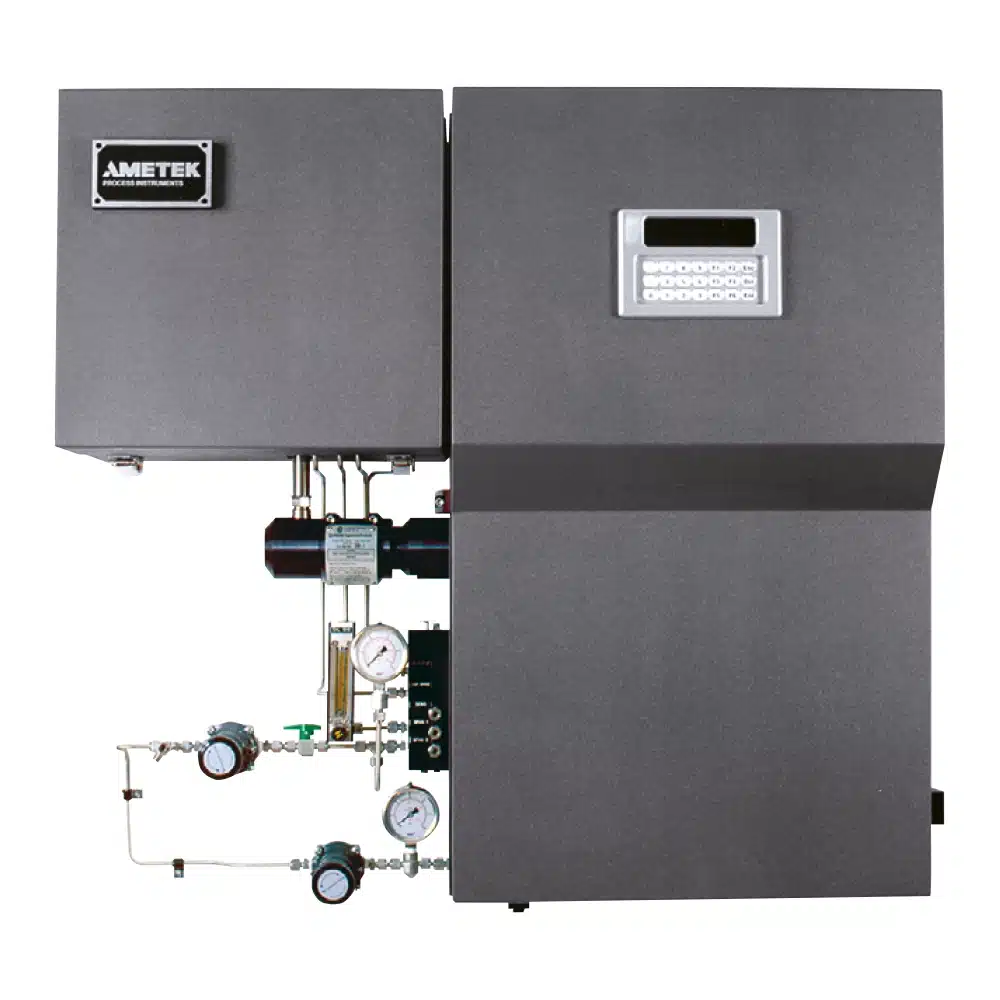
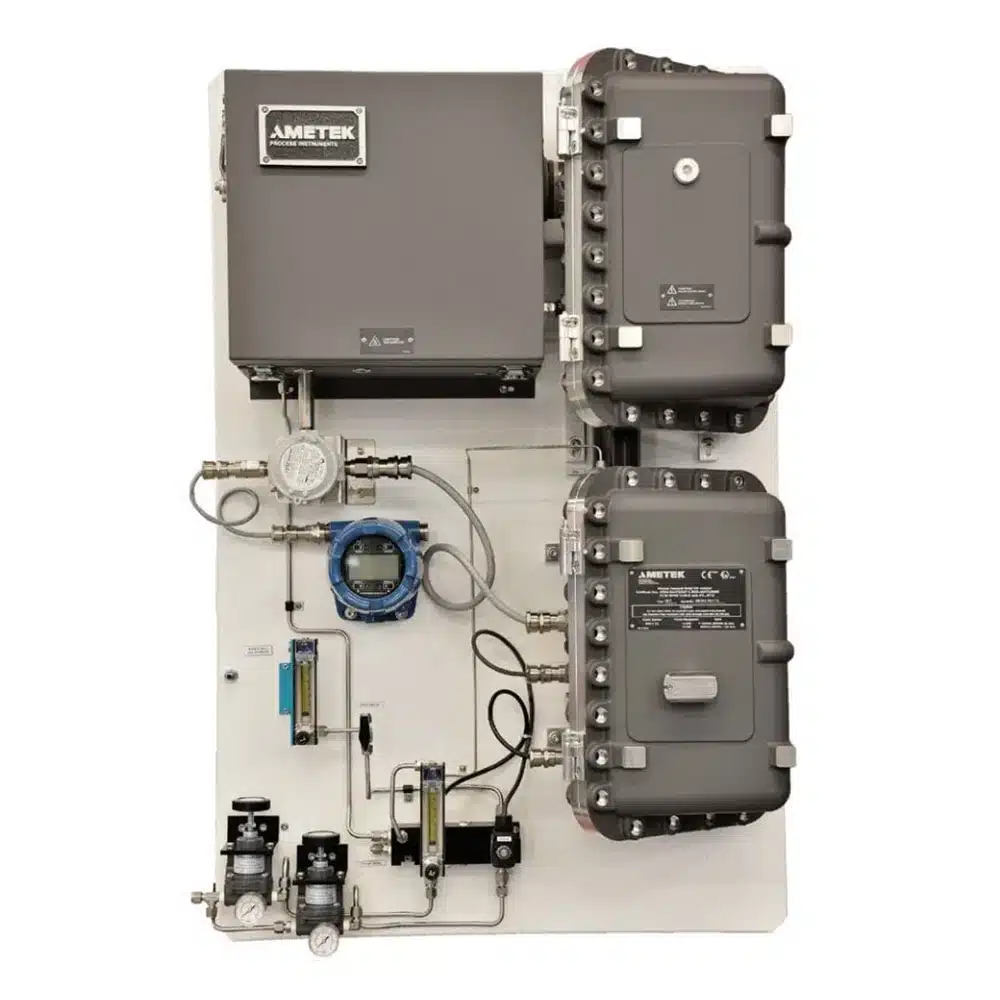
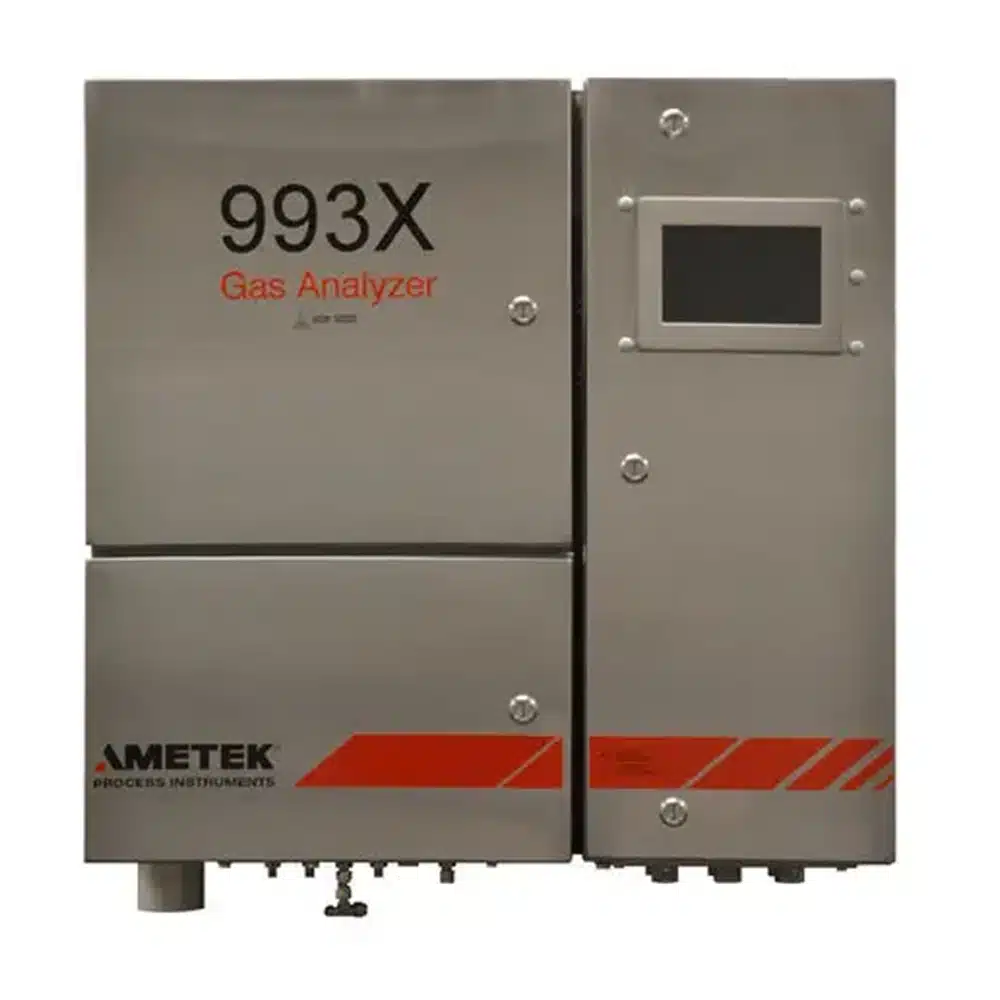
H2S and NH3 analyzer for loads in sulfur recovery plants, equipped with dual optical photometer for simultaneous measurement of HC. Equipped with a specific probe (ASR), it allows the sample to be returned directly to the process.
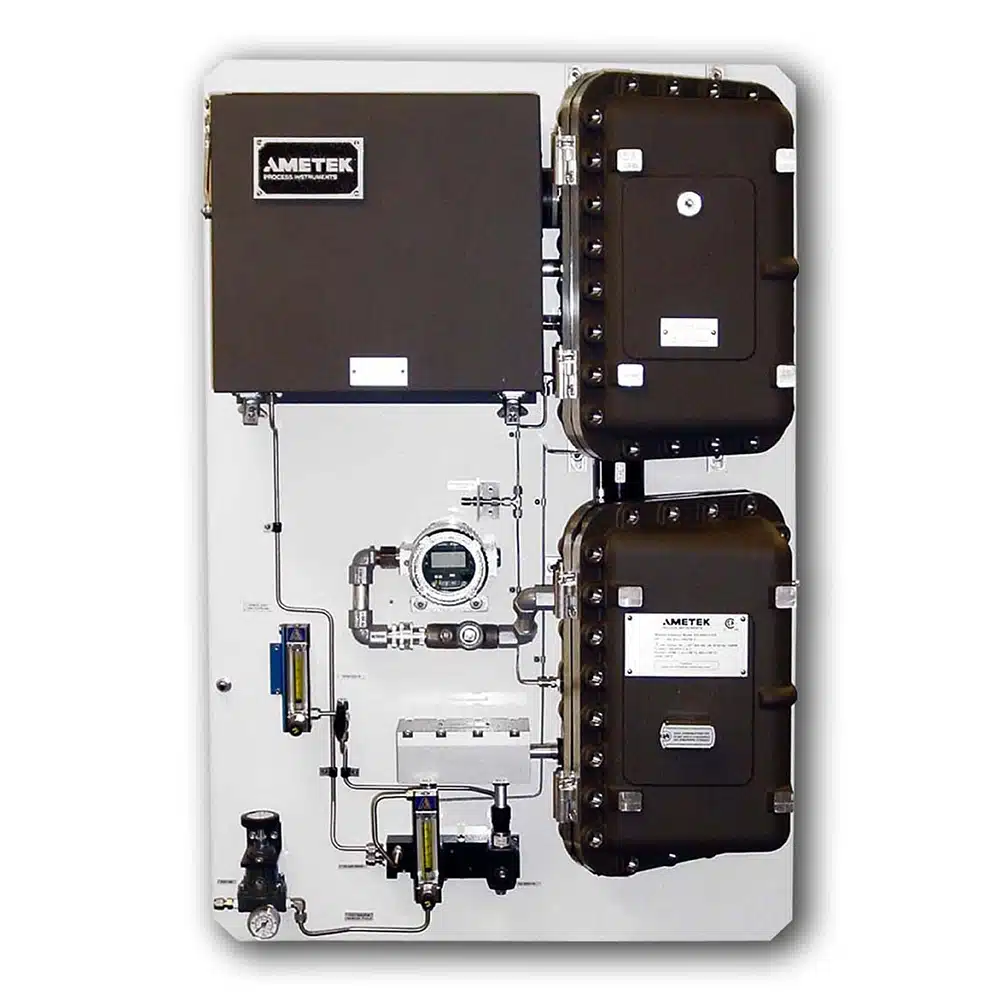
H2S (and H2) analyzer on Quench tower and Top Absorber for TGTU in Sulfur Recovery Plants. Equipped with a specific probe (ASR), it allows the sample to be returned directly to the process.
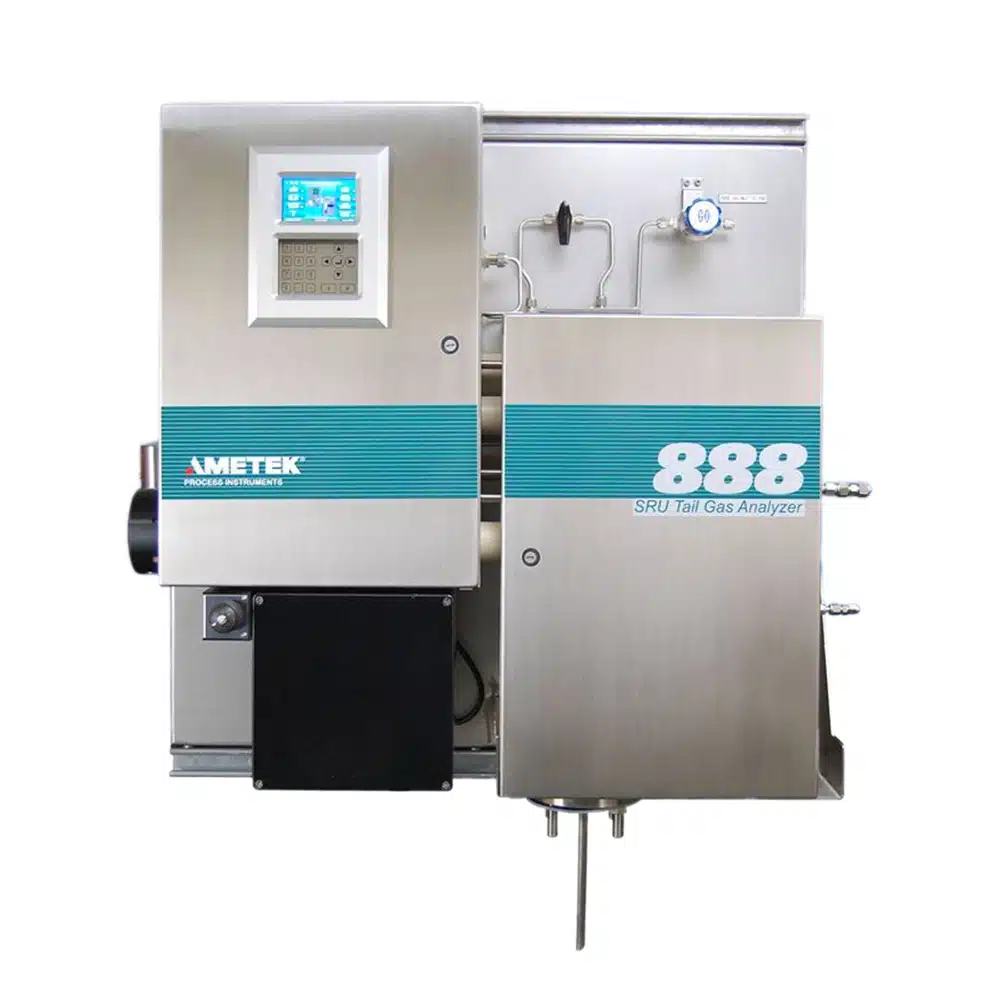
H2S/SO2 and Air Demand Analyzer on Tail Gas from Sulfur Recovery Plants, engineered for specific applications and equipped with built-in demister with sample return to process
Extractive analyzer for H2S/SO2, COS, CS2, and Air Demand on Tail Gas from Sulfur Recovery Plants, engineered for specific applications and equipped with built-in demister with sample return to process.
Specific H2 analyzer on Quench tower and Top Absorber for TGTU in Sulfur Recovery Plants. Equipped with a specific probe (ASR), it allows the sample to be returned directly to the process.
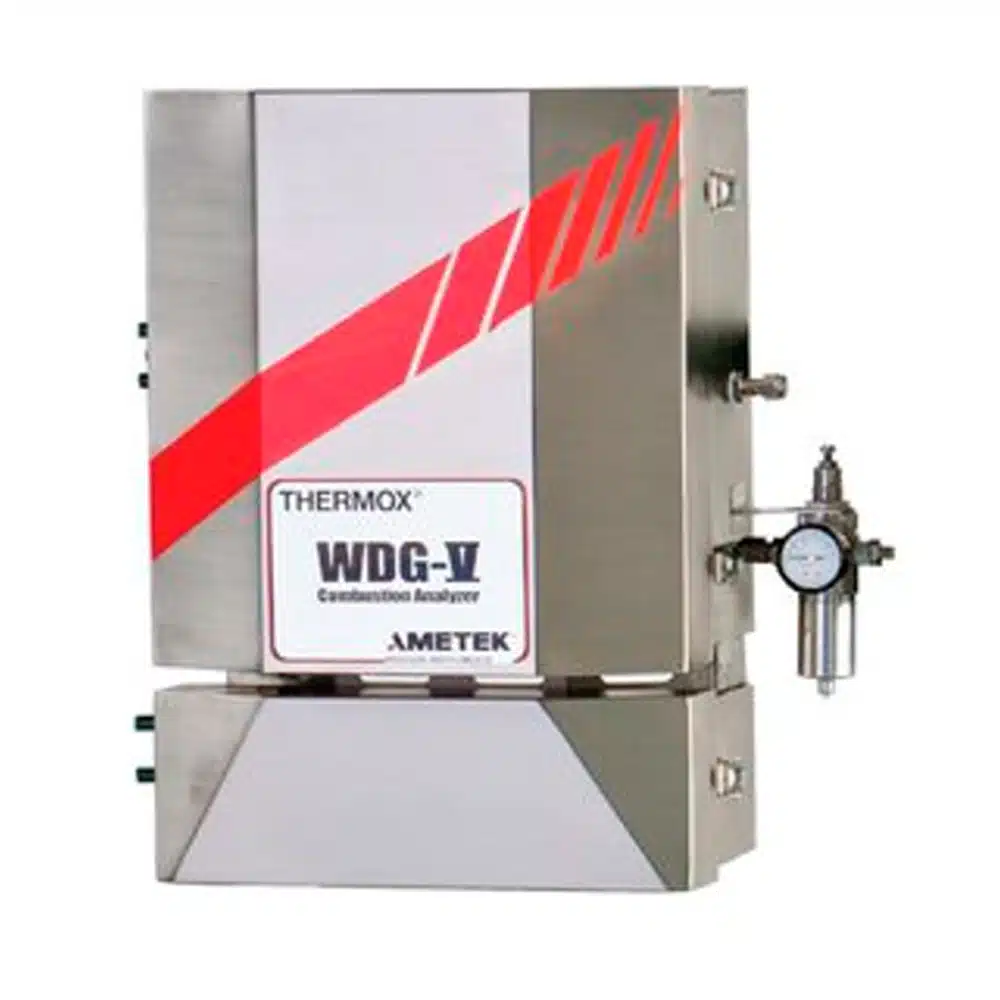
Combustion Gas Oxygen Analyzer, suitable for optimizing combustion in furnaces thanks to optional measurements of unburned gases (CO+H2) and methane. Suitable for operating with samples up to 1648°C.
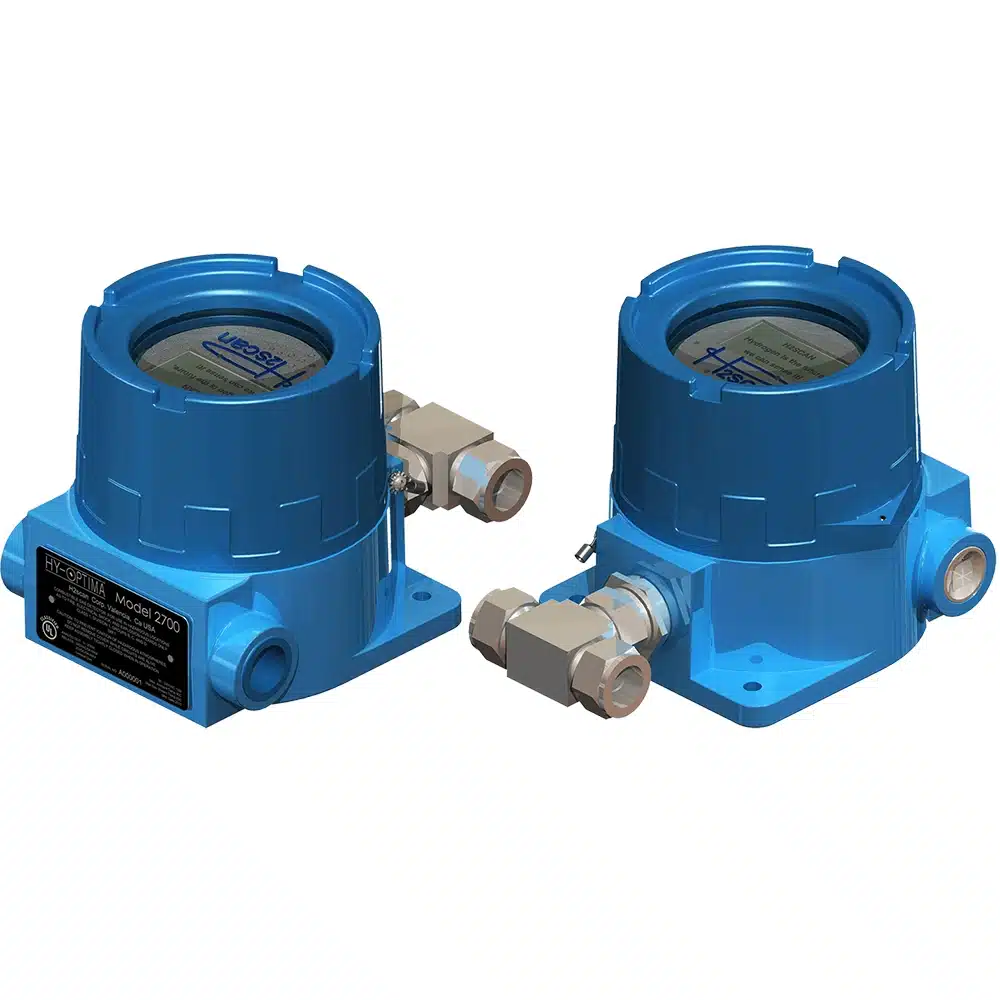
H2 analyzer equipped with Ni-Pa technology selective only to the H2 molecule, with a measuring range from 0.1 to 100%. Ideal for online and real-time measurement of hydrogen in complex mixtures, with high ease of use and flexibility for optimal process control.
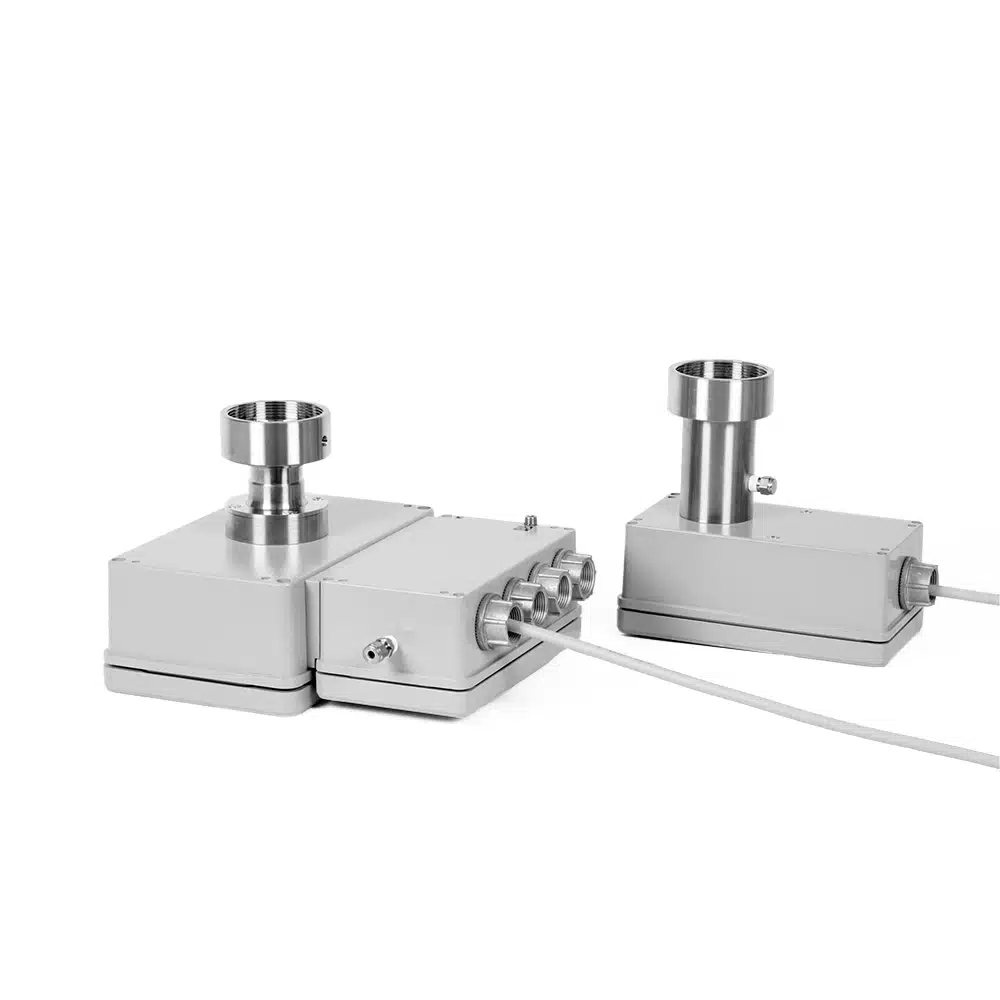
Derived from the standard single-path instrument. The compact monitor is optimized for short-distance measurement in the range from 10 to 100 centimeters. It is a non-contact optical measurement method, also known as in-situ.
LaserGas™ II SP Compact offers a wide range of gases, measurement ranges, and temperatures, as well as dual gas measurements. LaserGas™ II SP also has a wide range of Ex certifications, including IECEx, ATEX, and CSA. The instrument does not require consumables and does not need regular maintenance.
The absence of extractive conditioning systems further improves measurement availability and eliminates errors related to sample handling. Once the power supply, data lines, and purge are connected, the instrument is ready for use and measurements are performed in real time.
In addition, the physical dimensions are smaller than the LaserGas™ II SP.
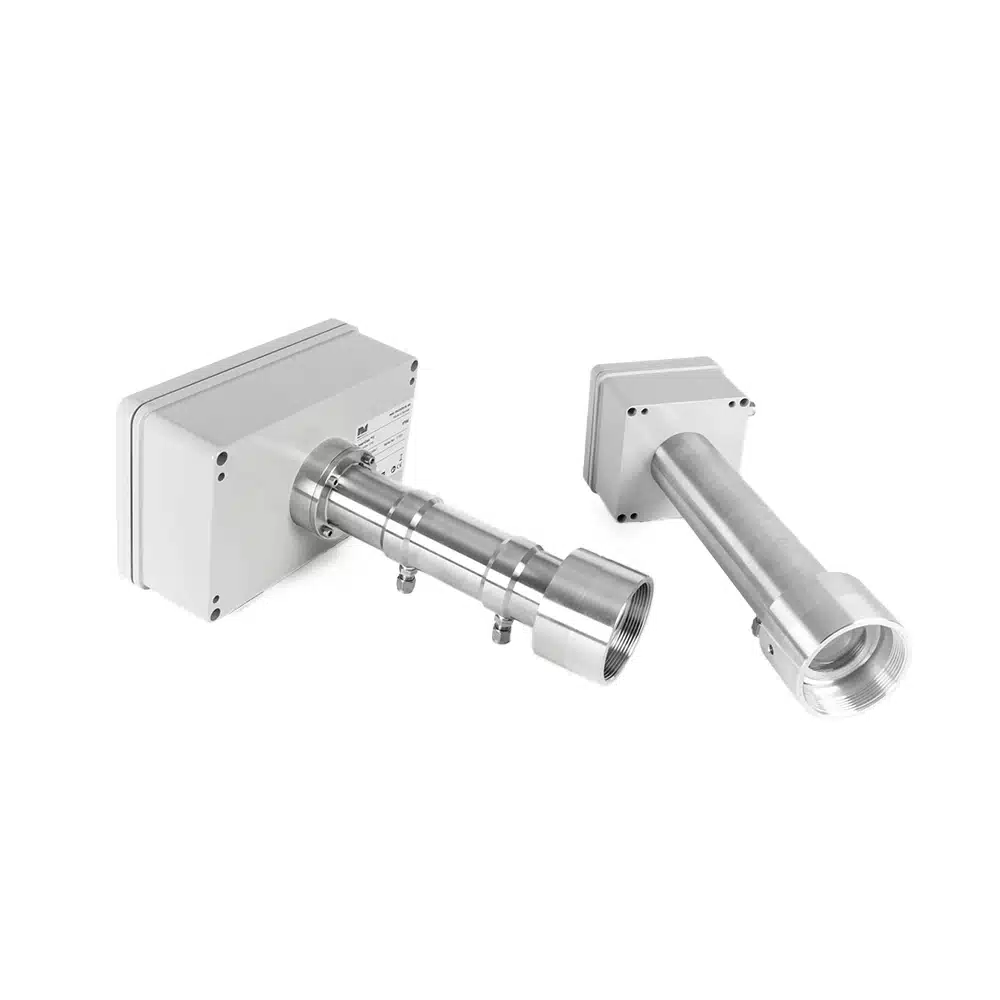
Neo Monitors is proud to offer the first in-situ optical analyzer for hydrogen.
The LaserGas™ II Single Path Hydrogen is a version specially designed for hydrogen measurement. The sensor is not affected by corrosive contaminants and does not require regular maintenance. The absence of extractive conditioning systems further improves measurement availability and eliminates errors related to sample handling.
Once the power supply, data lines, and purge lines are connected, the instrument is ready for use and measurements are performed in real time.